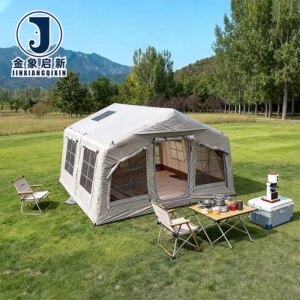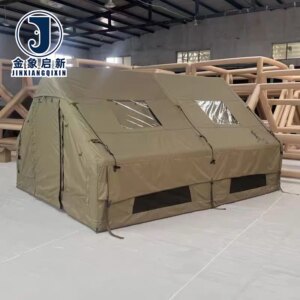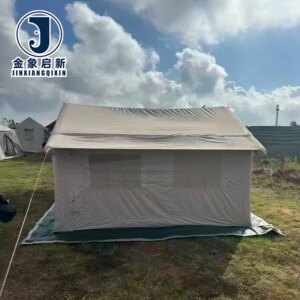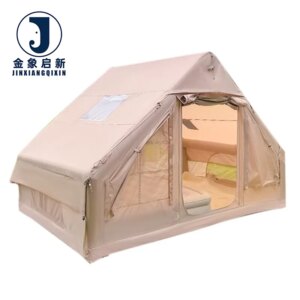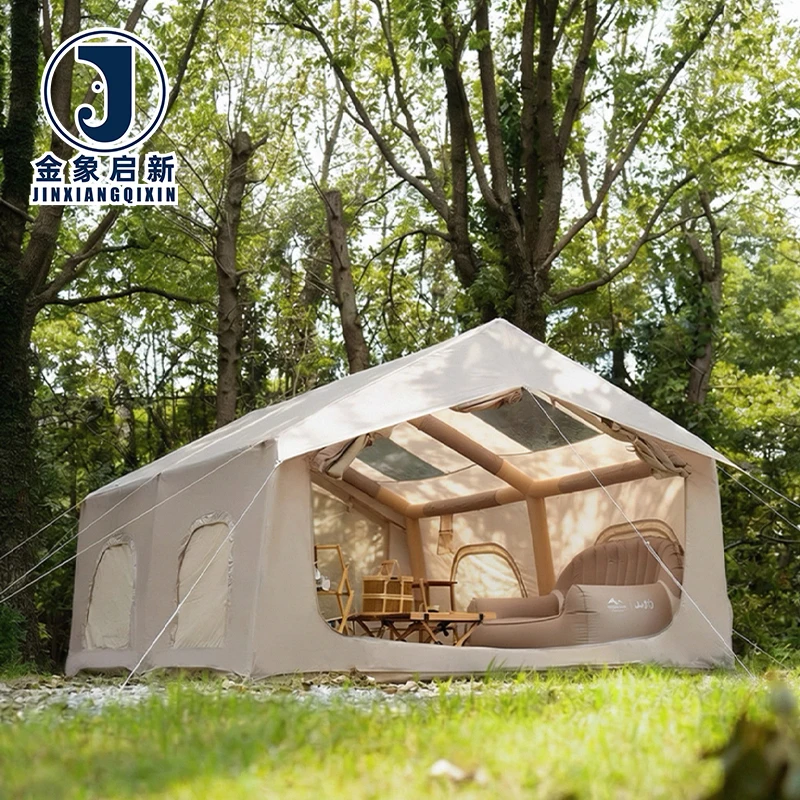
Three full production lines — supporting bulk PVC inflatable tent output with reliable on-time delivery for fleet and emergency logistics programs.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC tarpaulin |
| Key Features | Waterproof, UV-resistant, tear-resistant, fire-retardant, anti-static |
| Product Form | Inflatable structure with quick automatic opening |
| Certifications | ISO9001, ISO14001, ISO45001, CE |
| Customization | OEM & ODM, sample customization, pattern printing |
| Quality Control | 100% pre-shipment inspection, dedicated QA & QC staff |
Note: Flame-retardant and anti-static grades are available — confirm the grade required for your market. UV-resistant treatment is offered; request test documentation for verification.
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Truck-mounted emergency shelters | Road vibration, wind load during transit, rapid deployment on arrival |
| Disaster relief medical tents | Continuous weather exposure, floor-to-fabric abrasion, hygiene compliance |
| Fleet logistics support tents | Repeated inflation cycles, tie-down stress at anchoring points, UV from extended outdoor staging |
| Roadside incident cargo protection | Sudden deployment, contact with rough ground and debris, flame-retardant compliance near vehicles |
Why Inflatable Tent Fabric Fails at the Flex Points During Transit
Welded seams often give way before the fabric itself does — specifically where the load shifts and flexes against the trailer bed.
When transport fleets carry inflatable emergency shelters on flatbed trailers, the fabric undergoes constant low-amplitude flexing from road vibration and load movement. I have reviewed field returns where the PVC tarpaulin body remained intact but the seam lines — particularly at inflation chamber junctions — showed micro-cracking after just one convoy run. The issue is rarely the base fabric strength; it is the thermal weld quality and the reinforcement at stress concentration points. Without controlled heat-weld parameters matched to the coating weight, seams become the structural weak link. Fleet operators and transport equipment builders specifying inflatable tent fabric for transport and emergency deployment must ask for seam peel-strength data, not just fabric tensile figures [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421].
Reinforcement Strategy for Trailer-Mounted Shelter Units
Inflatable tent fabric for transport and emergency deployment faces a distinct mechanical profile compared to static installations. The anchoring interface between the tent base and the trailer deck must handle shear forces generated by braking and cornering. We construct tie-down attachment zones with additional PVC layers heat-welded over the primary shell, distributing point loads across a wider area of the base fabric. This approach prevents the common failure mode where a single grommet pulls through the coated fabric under dynamic load.
Quick-Opening Mechanism and Road Exposure Durability
The automatic inflation structure relies on airtight chamber integrity across the entire shell. During overland transport, even deflated and packed, the folded PVC tarpaulin is subject to compression against hardware, tie-down straps, and adjacent cargo. Coating adhesion must be sufficient to resist delamination at fold lines after repeated packing and deployment cycles. Our coating process controls the bond between the PVC layer and the base fabric to maintain chamber airtightness through these mechanical stress sequences [NEED_CITE: coating adhesion and peel strength testing for inflatable fabric structures].
How Coating Weight and Base Fabric Interact in Inflatable Structures
Inflatable tent performance depends on the relationship between the PVC coating weight and the underlying base fabric construction. The coating provides airtightness and waterproofing, while the base fabric — its denier and weave density — determines how the structure resists tearing under internal inflation pressure. A heavy coating on a loosely woven base may crack under flex, while a light coating on a dense base may fail to seal the chamber adequately. For transport applications, the balance must account for the vibration and flex cycles the fabric endures on a moving trailer, not just the static pressure of a deployed shelter. Surface finish also plays a role: a matte finish reduces glare during daytime deployment and provides better adhesion for printed fleet identification or emergency service markings.
What Happens When Flame-Retardant Grade Does Not Match Site Requirements
Emergency deployment sites — particularly those involving temporary medical operations or disaster relief near fuel stores — often require documented flame-retardant compliance before a shelter can be erected. I have encountered procurement cases where inflatable tents arrived on site with a general "flame retardant" label but no grade-specific test certificate. The result: the shelter was rejected by the site safety officer, the convoy was delayed, and a replacement order had to be expedited at considerable logistics cost. Batch-level documentation, not just supplier claims, is what gets a shelter through the site inspection [NEED_CITE: fire classification standards for temporary structures in emergency zones].
Why Procure Inflatable Tent Fabric Here
Our three full production lines and 36 sets of professional equipment handle the volume required for fleet-scale inflatable tent programs without sacrificing per-unit quality control. A 10-person R&D team develops custom sizing to match specific trailer bed dimensions and inflation chamber geometries, with samples produced within days. Every production stage includes dedicated QA and QC oversight, culminating in 100% inspection before dispatch — critical when a single defective chamber compromises an entire shelter unit. We support OEM and ODM requirements including pattern printing for fleet identification, and our coating process control ensures batch-to-batch consistency across multi-unit orders.
Documentation & Verification
- Material specification sheet stating PVC base fabric type, coating weight, and treatment details per batch
- Fire-retardant and anti-static test reports with applicable grade and standard clearly identified
- Pre-shipment inspection record covering seam integrity, airtightness, and dimensional accuracy
- ISO and CE certificates confirming management system and product compliance
- Roll and unit packing list matched to purchase order line items
Fabrication, Handling & Storage
- Heat-weld parameters must match the PVC coating weight to ensure seam peel strength at inflation chamber junctions
- Reinforce tie-down and anchor zones with additional welded PVC layers to distribute dynamic loads during transit
- Store packed inflatable units flat or on large-diameter cores to prevent permanent creasing of the coated fabric
- Avoid dragging deflated tents over abrasive surfaces; the PVC coating resists puncture but repeated abrasion degrades the surface
- Clean with mild detergent compatible with PVC coatings; solvent-based cleaners may attack the plasticizer in the coating layer
- Field repair of minor punctures requires PVC-compatible adhesive patches matched to the coating chemistry
What We Need to Specify Your Inflatable Tent Fabric
To match the correct PVC tarpaulin construction and treatment package to your transport and deployment requirements, we ask for the trailer model or bed dimensions, the inflation chamber layout you require, and the flame-retardant or anti-static grade your operating jurisdiction mandates. If your fleet standardizes on a specific colour or printed identification scheme, provide the colour reference and artwork so we can confirm batch consistency and print durability on the selected surface finish.
Frequently Asked Questions
Q: How is the inflatable tent sized to fit specific truck and trailer models?
A: We develop the tent footprint and chamber layout from the exact trailer bed dimensions and load profile you provide. The R&D team produces a sample for fitment verification before full production, ensuring the inflatable structure mounts correctly and secures properly during road transit without overhang or gap issues at the tie-down points.
Q: What tie-down and eyelet reinforcement options are available for transport loads?
A: We apply additional PVC layers heat-welded at anchoring zones to spread point loads across the base fabric. The reinforcement design accounts for the dynamic forces generated during braking and cornering on a flatbed trailer, preventing pull-through failures that occur with single-layer grommet installations.
Q: How are welded seams tested to withstand flex and vibration during transit?
A: Seam peel-strength testing is performed on welded samples from each production run. We verify that the thermal weld parameters match the coating weight so that chamber junctions resist the micro-flexing and vibration encountered during overland convoy transport without developing cracks or air leaks.
Q: What flame-retardant and anti-static certifications are provided for emergency deployment compliance?
A: We supply test reports stating the specific flame-retardant grade and anti-static standard achieved by the material batch. The documentation package includes the applicable test method and classification so your site safety officer can verify compliance against local emergency deployment regulations.
Q: How is batch colour consistency controlled when ordering multiple units for a fleet?
A: Colour matching is verified at the coating stage against your approved reference, and every unit in the order is inspected side-by-side before packing. This ensures that when multiple inflatable tents are deployed adjacent to each other at an incident site, no visible shade variation appears across the fleet installation.