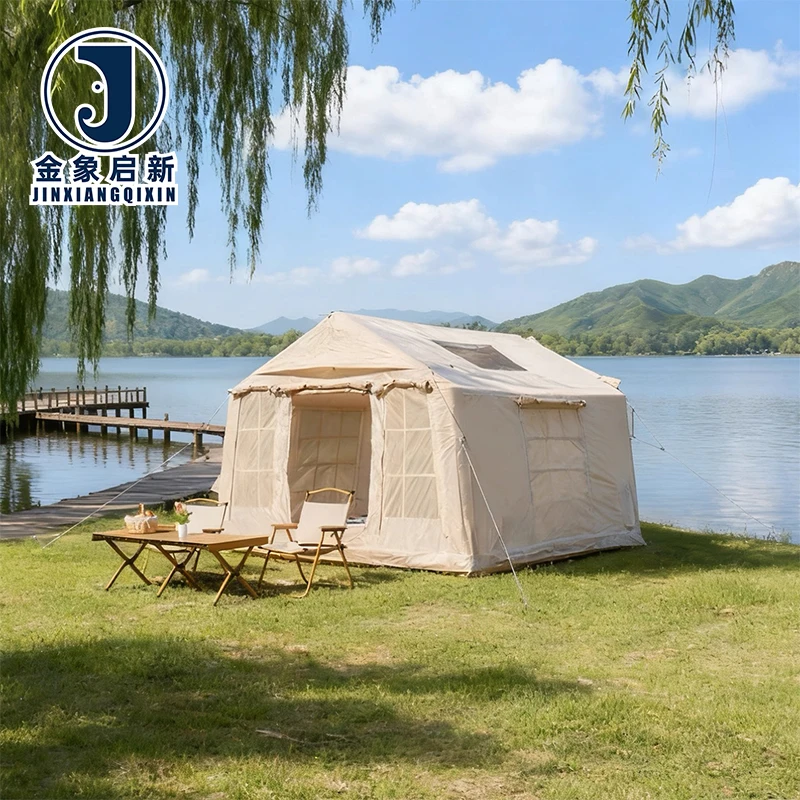
Coating Consistency Control — Every roll of PVC knife-coated inflatable tent fabric undergoes in-line thickness monitoring to maintain a tolerance of ±3%, verified against the stated specification before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC tarpaulin (PVC knife-coated fabric) |
| Thickness Range | 0.4–1.2 mm (custom selection by application) |
| Thickness Tolerance | ±3% batch-to-batch |
| Tear Strength | ≥300 N |
| Waterproof Rating | ≥5000 mm |
| Fire-Retardant Grade | UL94 V-0 |
| UV Resistance | Available in UV-resistant grades — confirm the grade required for your market |
| Anti-Static | Available in anti-static grades — confirm the grade required for your application |
| Key Features | Waterproof, UV-resistant, tear-resistant, fire-retardant, anti-static |
| Customization | OEM & ODM — size adjustment, thickness selection, pattern printing, structural modifications |
| Sample Lead Time | 7–10 days |
| Production Lead Time | 15–20 days (under 500 units); 25–30 days (larger or highly customized orders) |
| Certifications | ISO 9001, ISO 14001, ISO 45001, CE, UL94 V-0 |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Commercial outdoor gear manufacturing | Repeated inflation/deflation cycles demanding high tear strength and consistent seam adhesion under cyclic air pressure |
| Industrial team shelters and expedition base camps | Extended outdoor exposure requiring waterproof integrity and fire-retardant compliance for temporary structure permits |
| Disaster response and industrial temporary housing | Rapid deployment under field conditions where fabric must withstand abrasion during transport and setup on uneven terrain |
| Outdoor service provider branded tents | Custom pattern printing on knife-coated surface with colour consistency across multiple units for fleet branding |
Why Unverified Fire-Retardant Claims Put Your Inflatable Tent Product Line at Risk
A fire-retardant grade is only meaningful when backed by a test report tied to a specific standard and batch.
Commercial outdoor gear brands face mounting pressure from regulators and insurers to document the fire classification of every temporary structure in their catalogue. When the inflatable tent fabric arrives with only a "flame retardant" label and no UL94 V-0 test report, procurement teams cannot satisfy the compliance paperwork that event venues and municipal authorities demand. This gap delays product launches and erodes buyer trust across distribution channels. [NEED_CITE: UL94 V-0 vertical burn test method for plastic materials]
How the Inflatable Tent Fabric Manufacturer Custom Process Works
Sourcing Inflatable Tent Fabric manufacturer custom material begins with defining the inflation pressure, expected setup frequency, and the regulatory environment where the tent will operate. A 10-person R&D team reviews these inputs to recommend the appropriate thickness within the 0.4–1.2 mm range and selects the base fabric denier that balances tear strength with pack weight. Sample development proceeds within days, allowing buyers to test weld adhesion and air retention before committing to volume.
Controlling Thickness Variance Across Production Batches
Consistent wall thickness is critical for inflatable structures because uneven material creates stress concentrations that lead to premature seam failure during inflation. In-line caliper monitoring tracks coating weight across the full width of the web, holding tolerance to ±3% — a level of control that prevents the soft spots and over-thick ridges that compromise air chamber geometry. Each production run is logged with batch-specific readings so that reorders match the original specification exactly. [NEED_CITE: coated fabric thickness measurement methods per ISO standards]
Reading the Specs That Matter for Inflatable Applications
Tear strength of ≥300 N indicates the force required to propagate a rip through the PVC knife-coated fabric, which directly affects how the tent skin handles puncture events during field setup on rocky or debris-strewn ground. The knife-coating process bonds the PVC layer to the base fabric at a molecular level, producing higher peel strength than laminated alternatives — this adhesion is what keeps the air chamber walls intact through hundreds of inflation cycles. The waterproof rating of ≥5000 mm ensures that rain loading does not add unmanageable weight to the inflated structure, while the UL94 V-0 fire-retardant grade satisfies the classification required by most commercial and institutional buyers for temporary occupancy permits. Thickness selection within the 0.4–1.2 mm range allows designers to balance structural rigidity against pack size, with heavier grades suited to semi-permanent installations and lighter grades for expedition portability.
The Hidden Cost of Skipping Batch Verification
When inflatable tent fabric arrives with thickness that deviates beyond tolerance, weld parameters calibrated for the sample no longer produce reliable seams — the result is chambers that leak or burst during customer demonstrations. Colour shift between rolls forces manufacturers to sort and re-match panels, inflating labour costs and delaying shipment schedules. Fire-retardant fabric supplied without a traceable test report can fail site inspection, leaving an entire event shelter order rejected and the brand exposed to contractual penalties. [NEED_CITE: relationship between coating thickness variance and heat-seal integrity in coated fabrics]
Why Source Inflatable Tent Fabric From This Facility
Three dedicated production lines equipped with 36 sets of professional coating and finishing equipment provide the capacity to fulfil volume orders without sacrificing the batch-level QC that inflatable structures demand. The 10-person R&D team handles material selection, structural modification, and pattern printing in-house, reducing the back-and-forth between separate suppliers. A 9,180 m² production facility supports container-scale dispatch with documented pre-shipment inspection on every roll and cut piece. ISO 9001, ISO 14001, and ISO 45001 management systems ensure traceability from raw material receipt to final packing, giving buyers the audit trail that institutional procurement requires. Nearly 30 years of coated fabric process control translates into predictable material behaviour when your fabrication team dials in weld temperature and cycle time.
Documentation & Verification
- Material specification sheet confirming base fabric denier, PVC coating method, and thickness reference per batch
- UL94 V-0 fire-retardant test report issued against the specific production batch shipped
- Waterproof performance test record documenting hydrostatic head result for the material grade supplied
- Pre-shipment inspection report with dimensional and thickness measurements for each roll or cut piece
- ISO 9001, ISO 14001, ISO 45001, and CE certificates included with shipping documentation
Fabrication, Handling & Storage
- Heat-seal temperature and dwell time must be calibrated to the selected thickness within the 0.4–1.2 mm range to achieve full PVC layer fusion
- Seam allowance design should account for the ≥300 N tear strength by specifying adequate overlap at inflation stress points
- Store rolls upright on end-caps to prevent flat-spot creasing that compromises the knife-coated surface finish
- Allow cold-stored rolls to acclimatise before unrolling to avoid micro-cracking in the PVC coating at low temperatures
- Use PVC-compatible adhesives for field repair patches, matching the coating chemistry to ensure bond adhesion
What to Include in Your Inquiry
Provide the inflation pressure your design operates at, the target market’s fire classification requirement, and the annual volume you need to plan production slots. Specify whether you require roll stock in a standard width or pre-cut panels with custom dimensions and pattern printing. Indicate if pre-production samples are needed for weld parameter validation before bulk commitment.
Frequently Asked Questions
Q: How is material thickness verified on each batch before shipment?
A: In-line caliper monitoring tracks coating thickness across the full web width during production, holding variance to ±3%. Each batch is logged with specific readings, and the pre-shipment inspection record includes these measurements so buyers can verify conformance against the agreed specification before the material leaves the facility.
Q: What fire-retardant grade does the inflatable tent fabric carry?
A: The fabric carries a UL94 V-0 fire-retardant grade, which is documented through a batch-specific test report included with shipment documentation. Buyers targeting markets with different classification systems should confirm the required standard during inquiry so alternative grades can be evaluated.
Q: How do you control colour consistency across rolls in a single custom order?
A: Colour matching is managed through controlled pigment batching and in-line visual inspection under standardised lighting. Pre-shipment inspection records document colour readings per roll, and any variance outside tolerance triggers sorting before dispatch to ensure panels from different rolls install without visible mismatch.
Q: What OEM/ODM customization options are available?
A: Customization covers size adjustment, thickness selection within the 0.4–1.2 mm range, pattern printing, and structural modifications to chamber geometry. The 10-person R&D team develops samples within 7–10 days, allowing buyers to validate weld performance and inflation behaviour before authorising bulk production.
Q: What documentation is provided for international compliance and import clearance?
A: Each shipment includes a material specification sheet, UL94 V-0 test report, waterproof performance record, pre-shipment inspection data, ISO and CE certificates, packing list, and certificate of origin. Third-party testing through SGS or Intertek can be arranged on request to meet specific market entry requirements.