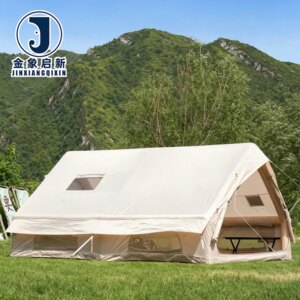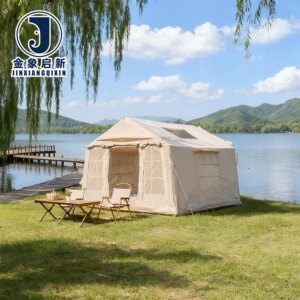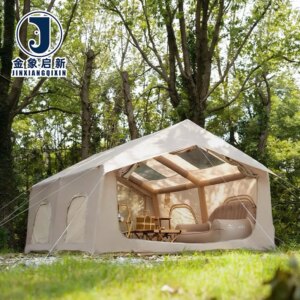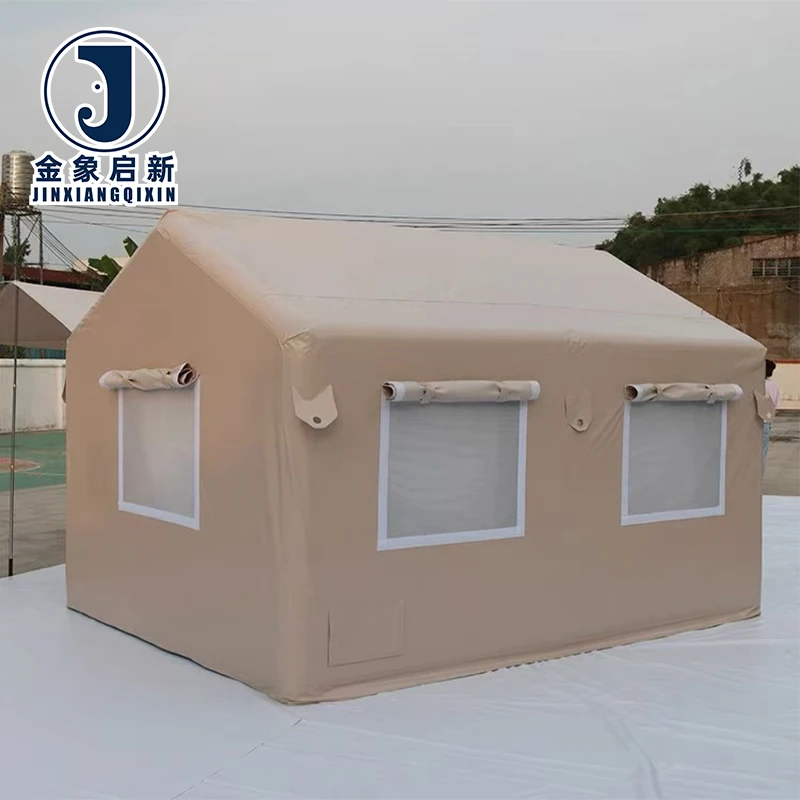
Coated Fabric Expertise — nearly 30 years focused on PVC inflatable tent fabric development, with dedicated QA at every production stage ensuring material integrity from coating to dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC tarpaulin |
| Product Forms | Inflatable structure |
| Waterproof | Fully waterproof coated construction |
| UV Resistance | Available in UV-resistant grades — confirm the UV standard required for your market |
| Fire Retardant | Available in flame retardant grades — confirm the grade required for your market |
| Anti-Static | Available in anti-static grades — confirm the anti-static standard required for your site |
| Tear Resistance | Tear-resistant construction |
| Customization | OEM & ODM: sample customization, pattern printing, material selection, product design |
| Production Lines | 3 full production lines |
| Processing Equipment | 36 sets of professional processing equipment |
| R&D Team | 10 technicians |
| Certifications | ISO9001, ISO14001, ISO45001, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Temporary site offices | Wind loading on inflatable beams, daily entry abrasion, prolonged sun exposure |
| Equipment storage shelters | Water ingress protection, dust sealing, repeated inflation-deflation cycles |
| Mobile field operations | Rapid deployment under variable weather, transport abrasion, ground contact wear |
| Construction sites | Debris impact, chemical splash exposure, compliance-grade fire retardancy |
| Outdoor event management | Crowd-proximate fire safety requirements, UV fade resistance across event seasons |
| Industrial project bases | Four-season temperature fluctuation, high-wind structural loading, continuous occupancy |
Why Inflatable Tent Fabric for Transport and Structural Application Demands More Than a Data Sheet
The weld line — not the fabric itself — is where most inflatable structures fail under operational load.
When procurement teams evaluate PVC inflatable tent material, the conversation often stops at weight per square metre and a generic waterproof claim. Yet inflatable structures concentrate stress at the seams where air beams meet the shell, where tie-off points transfer wind load, and where the base fabric folds during packing. Generic material without verified weld adhesion or confirmed fire retardant grading creates exposure that only surfaces once the structure is inflated on site. [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]
Coating Adhesion and Air-Beam Integrity
Inflatable tent structures depend on continuous air pressure to maintain form. The PVC tarpaulin used in these applications must sustain internal pressure across welded seams that flex with every inflation cycle. Material with insufficient coating adhesion will delaminate at the beam joints long before the base fabric reaches its tensile limit, causing slow deflation that operators may not detect until the structure visibly sags.
Fire Compliance Across Jurisdictions
Construction and event sites increasingly require documented fire retardant classification before any temporary structure is permitted on the ground. PVC inflatable tent fabric can be formulated with flame retardant additives, but the grade must match the specific standard enforced at the project location — a B1 rating under one framework does not automatically satisfy a different local authority’s requirement. Buyers must confirm the applicable standard before production begins. [NEED_CITE: fire classification standards for temporary structures in construction environments]
Reading the Specifications That Matter
PVC tarpaulin weight per square metre indicates coating volume, but tensile and tear performance are governed equally by the base fabric denier and weave density. A heavier coat on a loosely woven scrim will not outperform a lighter, tightly woven base when a tear initiates at a puncture point. Coating method — whether knife-over-roll, laminated, or calendered — directly affects peel strength at welded seams and determines which heat-sealing parameters the fabric will accept without scorching or incomplete bonding. Surface finish, glossy or matte, influences how readily the material sheds dirt and accepts printed graphics, while also affecting how the fabric behaves when folded tightly for transport.
The Cost of Overlooking Weld Performance
Inflatable structures that fail at the seam rather than the fabric body create a specific operational problem: the material itself appears intact, yet the structure cannot hold pressure. This failure pattern typically traces back to either incorrect welding temperature for the specific coating formulation or material where the coating-to-substrate bond was never tested for peel strength under cyclic flexing. On a construction site, this means a shelter that deflates overnight and delays morning operations, with no visible damage to point at for a warranty claim. [NEED_CITE: peel strength testing methods for coated fabric weld lines]
Sourcing PVC Inflatable Tent Fabric With Verified Process Control
Coating weight consistency is maintained through continuous inline monitoring across all three production lines, preventing the variation that causes colour and weight drift between rolls in a single shipment.
Each production run of PVC inflatable tent material undergoes in-process QA checks at coating, curing, and winding stages, with a dedicated team assigned to catch deviations before the roll leaves the line.
A 10-technician R&D team supports material selection for specific inflation pressures and structural geometries, developing sample runs that confirm weld parameters before bulk production is authorised.
Pattern printing and custom sizing are handled on the same production equipment, eliminating the coordination failures that occur when printing is subcontracted away from the coating facility.
Pre-shipment inspection covers every roll produced against the order specification, with findings documented before dispatch rather than sampled after packing.
Documentation & Verification
- Material specification sheet stating PVC tarpaulin composition, coating type, and weight for each inflatable tent fabric roll
- Test report for UV-resistant and flame retardant grades where applicable, matched to batch number
- ISO9001, ISO14001, ISO45001, and CE certificates covering the inflatable tent production facility
- Pre-shipment inspection record confirming weld adhesion and dimensional accuracy per order
- Roll packing list with individual roll identification for traceability through fabrication
- Certificate of origin and customs documentation for international inflatable tent material shipments
Fabrication, Handling & Storage
- Confirm heat-sealing temperature range for the specific PVC tarpaulin coating before welding inflatable beam seams
- Allow fabric to acclimatise before inflation in cold conditions to prevent coating stiffening at fold lines
- Store rolls horizontally on padded racking to prevent permanent creasing in the PVC tarpaulin coating layer
- Use compatible PVC-based repair adhesives for field patches on inflatable tent beam and shell damage
- Avoid solvent-based cleaners on matte-finish surfaces to prevent gloss variation across repaired panels
- Plan cutting layout to minimise transverse welds across inflatable beam axes where flex load concentrates
Specifying PVC Inflatable Tent Fabric for Your Project
Buyers evaluating PVC inflatable tent fabric for transport and structural application should provide the intended deployment environment, including wind load expectations and temperature range. Specify whether fire retardant or anti-static certification is required and which standard applies at the project site. Confirm whether you need raw fabric by the roll or finished inflatable structures with custom sizing and pattern printing, and indicate the target order volume to align production scheduling.
Frequently Asked Questions
Q: What fire retardant documentation ships with inflatable tent fabric orders?
A: Where flame retardant grades are specified, the shipment includes a test report referencing the applicable standard and the production batch. Confirm the fire classification required by your site authority before ordering, as different jurisdictions enforce different frameworks and the grade must be matched at the formulation stage to ensure compliance documentation is valid.
Q: How is batch-to-batch colour consistency controlled across inflatable structures?
A: Colour matching is verified against a reference standard at the coating stage, with inline monitoring across all three production lines. Each roll in an inflatable tent order is inspected before packing to confirm it falls within the accepted colour tolerance, preventing visible variation when multiple panels are installed adjacent to one another on site.
Q: How are welded seams at flex points tested before dispatch?
A: Welded seam samples are subjected to peel strength testing that simulates the cyclic flexing an inflatable beam experiences through repeated inflation and deflation. This identifies coating adhesion failures that would not appear in a static tensile test, ensuring the seam outlasts the fabric body under operational conditions.
Q: What are the sample and lead time arrangements for custom inflatable tent projects?
A: Sample development is handled by the 10-technician R&D team, with material selection, custom sizing, and pattern printing confirmed through physical samples before bulk production is authorised. Lead times depend on the degree of customisation and order volume, and are confirmed at the quotation stage after sample approval.
Q: What documentation accompanies shipment for customs and compliance purposes?
A: Each inflatable tent fabric shipment includes a material specification sheet, applicable test reports, ISO and CE certificates, a pre-shipment inspection record, a detailed roll packing list, and a certificate of origin. Additional customs support documentation is provided based on the destination country’s import requirements.