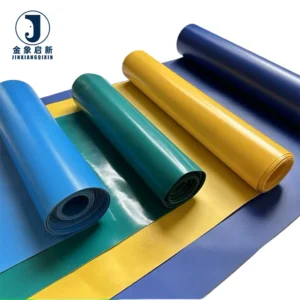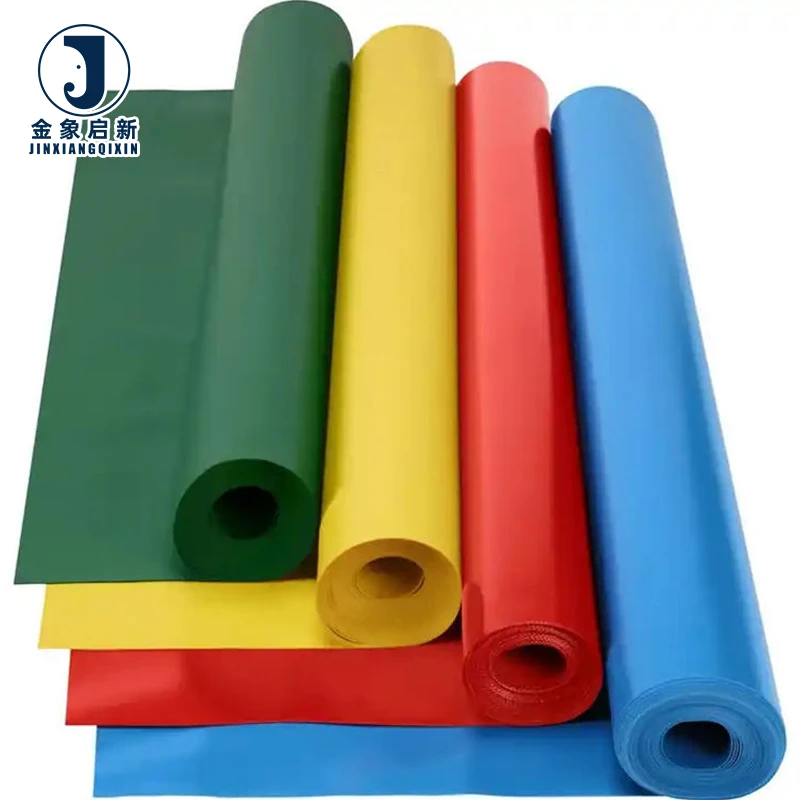
Batch-Matched Roll Stock — Every roll of 500D500D 1817 PVC tarpaulin is checked for GSM, colour and coating adhesion before dispatch, so fabricators receive consistent material across an entire order.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Coated Tarpaulin Roll |
| Base Fabric Denier | 500D*500D |
| Weave Count | 18*17 |
| Material | PVC Coated Polyester |
| Key Features | Fire Retardant, UV Resistance, Antibacterial, Mildew Proof, Oil and Stain Resistance, Acid and Alkali Resistance |
| Temperature Resistance | High Temperature and Cold Resistance |
| Flexibility | Highly Flexible, Resistant to Cracking |
| Welding Options | HF, Hot Air, Sewing |
| Surface | Self-Cleaning |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Tensile membrane structures | Continuous UV exposure, wind load cycling, long-term dimensional stability |
| Stadium architectural roofs | High wind uplift, pooled rainwater drainage, fire code compliance for public assembly |
| Airport hangar covers | Chemical and fuel vapour contact, large unsupported spans, flame safety standards |
| Portable storage structures | Repeated assembly and disassembly, abrasion at frame contact points, UV and mildew exposure |
| Shade systems and canopies | Direct solar radiation, thermal expansion and contraction, colour retention over seasons |
Why Stated GSM Is Only Half the Story for PVC Tarpaulin Roll Buyers
Coating weight and base fabric construction must both be verified, because GSM alone cannot predict how the material performs at the seam.
When a PVC tarpaulin roll aftermarket supplier quotes a weight, that figure combines the polyester base and the PVC coating together. Two rolls can carry the same GSM yet behave entirely differently on the welding table — one may have a heavier base with a thinner coat, the other a lighter base buried under thick coating. The second will feel stiff in cold weather and may crack at the fold, while the first will hold a weld line more reliably. Buyers who specify only by GSM often discover after delivery that the material does not match the performance they expected for tensile structures or shade canopies [NEED_CITE: coating-to-base weight ratio effects on coated fabric welding behaviour].
Colour Matching Across the Roll Run
When a membrane structure requires multiple panels installed side by side, even a slight shade difference between rolls becomes visible once the sun hits the surface. Our dye lots are tracked per order so that every roll of 500D*500D PVC tarpaulin fabric cut for a single project carries the same colour reference. If you reorder months later, a retained sample allows us to match the new batch against the original. This eliminates the situation where a shade canopy or stadium roof shows a patchwork appearance after installation.
Weld Behaviour at Flex Points
Tensile and shade structures place repeated stress on welded seams wherever the fabric bends around a cable or frame member. The 500D500D base with 1817 weave provides a stable substrate for high-frequency, hot-air and sewn joints. HF welding bonds the PVC coating layers directly, producing a seam that typically matches the fabric tensile value at the joint line [NEED_CITE: HF versus hot air weld strength comparison for PVC coated polyester]. Sewing with sealed thread offers an alternative where field repairs may be needed.
What the Base Fabric Construction Actually Controls
The 500D500D denier and 1817 weave count together determine how load distributes across the polyester grid. A higher denier yarn resists initial puncture, while the weave density governs how quickly a tear propagates once the surface is breached. In shade systems and tensile roofs, where wind gusts create sudden point loads, this combination provides balanced tear resistance without excessive material stiffness. The PVC coating then adds environmental protection — UV resistance, mildew proofing, and the self-cleaning surface that reduces maintenance on elevated structures where access is difficult.
The Hidden Cost of Overlooking Weld Compatibility
A roll that welds cleanly on one fabricator’s hot-air machine may delaminate on another’s if the coating formulation differs between suppliers. We supply PVC tarpaulin roll stock with documented coating characteristics so your production team can set temperature and speed parameters with confidence. When a membrane roof panel fails at the seam rather than the field of the fabric, the entire installed section must come down for rework — a cost that far exceeds the effort of confirming weld compatibility before production begins [NEED_CITE: seam failure frequency in tensioned membrane structures].
Consistent Supply for Roll-to-Roll Fabricators
Three full production lines and 36 sets of professional equipment allow us to maintain stock grades of 500D*500D PVC coated tarpaulin for regular buyers. A 10-person R&D team handles colour development, custom width requests and sample preparation within days. Dedicated QA/QC stages verify GSM, coating adhesion and colour at every roll before packing. ISO and CE certified processes underpin documentation that your compliance team can file directly.
Documentation & Verification
- Material specification sheet stating GSM, 500D500D base fabric, 1817 weave and PVC coating type
- Fire retardant and UV test reports matched to the dispatched batch
- Pre-shipment inspection record with roll-by-roll GSM verification and colour check
- Roll packing list with individual roll numbers for traceability
- Certificate of origin and customs support documentation for export shipments
Fabrication, Handling & Storage
- Set HF welder temperature to the PVC coating range; confirm bond strength on a 500D*500D scrap piece first
- Store rolls upright on end caps to prevent flat-spot deformation of the 18*17 weave base fabric
- Unroll in temperatures above freezing to avoid cracking the PVC coating at the fold line
- Use a mild pH-neutral cleaner on the self-cleaning surface; abrasive solvents will damage the topcoat
- Plan panel cutting layout to maximise roll width utilisation and minimise offcuts from the 500D*500D stock
Tell Us What the Project Demands
Share the intended structure type, span dimensions and the environmental conditions the fabric will face — coastal salt air, high-altitude UV, or industrial chemical exposure each affect coating selection. Let us know your target market so we can align fire retardant documentation with local building codes. Specify required roll widths, annual volume and whether you need stock colours or a custom shade developed against your reference sample.
Frequently Asked Questions
Q: How is GSM verified before shipment, and do I receive a per-roll record?
A: Each roll is weighed and measured individually during pre-shipment inspection. The inspection record lists the measured GSM alongside the quoted value for every roll number in your order, so you can confirm consistency before the container is sealed.
Q: Can I get fire retardant and UV test reports specific to my batch?
A: Yes. Test reports are issued per production batch, not as a generic datasheet. The fire retardant and UV resistance results reference your specific roll numbers, which satisfies site inspectors who require traceable documentation.
Q: What minimum order applies for custom width or colour, and how does lead time compare to stock rolls?
A: Custom widths and colours carry a minimum that varies by specification. Our R&D team prepares a sample within days for your approval. Lead times for custom runs extend beyond stock availability, which we confirm at the quotation stage.
Q: Will colour match if I reorder the same reference months later?
A: We retain a physical sample from every dye lot. When you reorder, the new batch is matched against that retained reference before production, keeping shade variation within tolerance across separate orders.
Q: Which welding methods work best with this fabric, and does seam strength hold at flex points?
A: High-frequency, hot-air and sewing are all compatible with the 500D*500D PVC coated construction. HF welding typically produces the strongest bond at flex points, and we provide coating parameters so your team can dial in machine settings before full production.