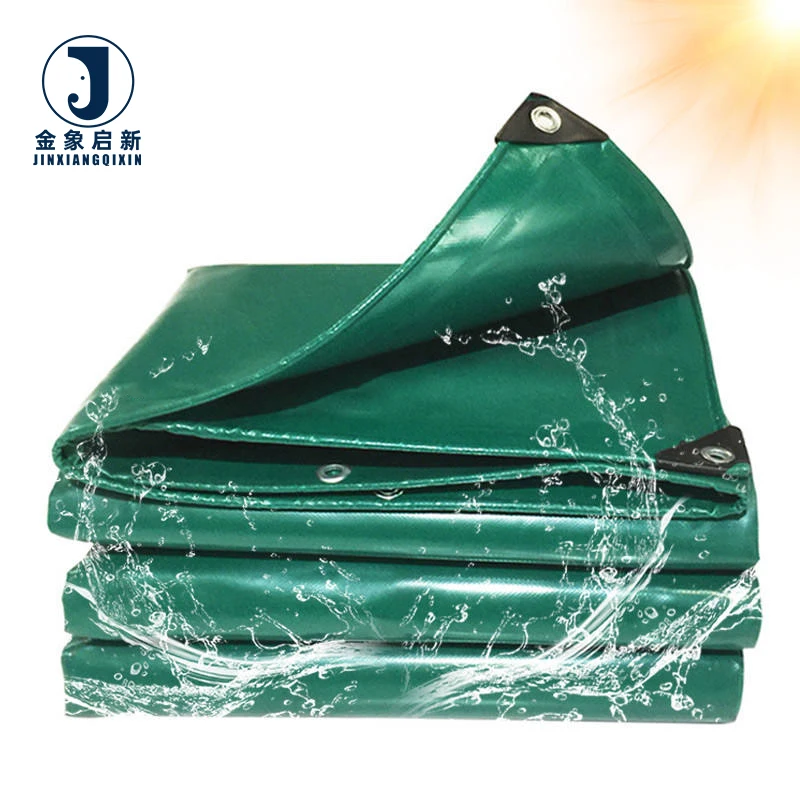
Deep Process Control Over Coating — Verified GSM and base fabric denier matching from coating to dispatch, addressing the flex-point failures that plague generic transport covers.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Coated Tarpaulin |
| Weight (GSM) | 350 / 400 / 420 / 500 / 600 / 650 / 750 / 900 |
| Base Fabric Denier | 500D840D / 500D1000D / 1000D1000D / 1000D1300D / 1300D1300D / 1000D2000D |
| Mesh Count | 3019 / 2020 / 30*15 |
| Total Thickness | 0.29mm / 0.32mm / 0.38mm / 0.44mm / 0.46mm / 0.55mm / 0.65mm |
| Tensile Strength (Warp) | 1650N to 3900N (test standard not stated in source) |
| Tensile Strength (Weft) | 1600N to 3500N (test standard not stated in source) |
| Coating Material | PVC |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| UV Treatment | Available with UV treatment — test basis not stated in source |
| Anti-Mildew | Claimed |
| Finish | Self Clean, Flexible |
| Temperature Range | Brittle temperature ≤ -50~-60 ℃; Softening temperature ≥ 80 ℃; Melting point 212 ℃ |
| Density | 1.15-2.00 g/cubic centimeter |
| Edge Reinforcement | 5mm thick rope without splicing, high temperature heat sealed seamless edge wrapping |
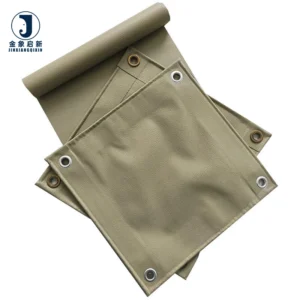
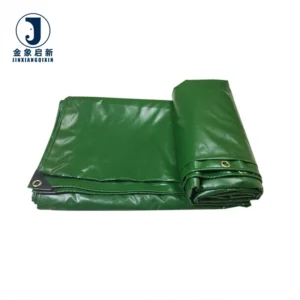
| Eyelets | 3cm enlarged aluminum alloy buttonhole, brass eyelets every 1 meter |
| Corner Reinforcement | Reinforced corners on all sides |
| Fabrication | High frequency hot melt, Hot air, Sewing |
| Printing | Printable, Customized |
| Standards | ISO, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Truck and Trailer Side Curtains | Constant flexing during transit, road abrasion at contact points, prolonged UV exposure, high-speed wind load |
| Top Roof Covers for Transport | Direct rainfall and pooling water, thermal cycling from sun exposure, tension from tie-down straps |
| Pallet and Equipment Covers | Repeated handling and folding, abrasion from load surfaces, forklift contact during loading |
| Container Roofs | Salt-laden air in port environments, sustained UV degradation, high wind uplift forces |
Why Welded Seams Fail Before the Fabric on Moving Loads
Heat-sealed edge wrapping with high adhesion prevents the glue cracking and loose edges that cause early seam failure on truck covers.
When a PVC coated tarpaulin for truck and trailer cover is strapped over a shifting load, the highest stress concentrates at the welded seams and eyelet zones. Generic fabrication often leaves these points under-engineered relative to the base fabric strength. The result is a cover that tears at the weld line or pulls away from the eyelet long before the main body shows wear. Fleet operators then face the cost of replacement mid-contract rather than at the planned service interval. [NEED_CITE: common failure modes in heavy-duty transport tarpaulins at flex points]
Reinforcement at the Points That Take the Load
The PVC coated tarpaulin for truck and trailer cover in this range is built with 3cm enlarged aluminum alloy buttonholes set into reinforced corners on all sides. Brass eyelets are spaced every 1 meter along the perimeter. This hardware specification addresses the tie-down forces that fleet operators apply daily, distributing strap tension across a broader fabric area rather than concentrating it at a single point.
Seam Construction Built for Flex Cycling
High temperature heat sealed seamless edge wrapping is applied with a 5mm thick rope without splicing embedded inside the hem. This construction method avoids the brittle glue lines that crack after repeated flexing in cold conditions. The rope core maintains hem integrity even when the cover is folded tightly for storage between loads, which is a frequent cause of edge failure on standard fabricated covers. [NEED_CITE: thermal welding parameters for PVC coated polyester fabrics]
Reading the Specification Beyond the GSM Number
GSM tells you the weight per square meter, but the base fabric denier and mesh count determine how that weight translates into structural performance. A 650 GSM cover built on 1000D1300D with 2020 mesh delivers different tensile behaviour than a 650 GSM cover on a lighter base with higher mesh density. The thicker denier yarns in the 1300D1300D construction resist tear propagation at stress points, while the tighter mesh count of 3019 in the 500D*840D option provides a smoother coating surface for printing. Selecting the right combination depends on whether the priority is tear resistance for heavy equipment covers or surface quality for branded side curtains. The coating adhesion, achieved through controlled PVC application, must also match the fabrication method — high frequency hot melt welding demands consistent coating thickness to produce reliable seam bonds.
The Hidden Cost of Specifying by Weight Alone
A truck cover ordered at 500 GSM may arrive measuring lighter than the quotation stated, a discrepancy that only becomes visible when the cover fails prematurely under load. Colour variation between rolls in the same shipment becomes apparent once installed side by side on a fleet of trailers, forcing either acceptance of an inconsistent appearance or a costly full replacement. Covers cut to generic dimensions rather than the specific trailer model leave excess fabric that flaps in transit, accelerating wear at contact points and creating noise complaints from drivers. [NEED_CITE: GSM verification methods and acceptable tolerance ranges for coated fabrics]
What Consistent Production Delivers for Fleet Procurement
Three full production lines with dedicated quality control at each stage mean that GSM, coating weight, and colour are verified roll by roll rather than sampled from batch averages. The 10-person R&D team develops samples within days for custom width, colour, or print requirements, allowing fleet operators to confirm fitment on actual trailer models before committing to production volume. Pre-shipment inspection covers every roll before dispatch, so what arrives at the depot matches the material specification sheet that accompanied the quotation. This process control eliminates the guesswork that typically accompanies bulk tarpaulin procurement for transport fleets.
Documentation & Verification
- Material specification sheet stating GSM, base fabric denier, mesh count and colour reference per roll
- Pre-shipment inspection record with verified weight measurement against quoted specification
- Test report for flame retardant or UV treatment where applicable, with stated grade and basis
- Roll packing list with individual roll identification for traceability through the supply chain
- ISO and CE certificates confirming manufacturing system compliance
- Certificate of origin and customs documentation for international shipment
Fabrication, Handling & Storage
- Heat-sealed seams on 500 GSM and above grades require consistent hot air temperature to achieve full coating bond
- 3cm aluminum alloy buttonholes should be set with reinforced PVC patches on high-tension zones
- Rolls of 0.55mm thickness and above should be stored upright to prevent permanent crease marks
- Cold-weather deployment below -20 ℃ requires gradual unfolding to avoid brittle coating fracture
- Self-clean finish surfaces tolerate mild detergent cleaning without degrading the coating layer
- Custom width rolls should be unrolled flat before cutting to allow material relaxation
Getting the Specification Right for Your Fleet
To specify the correct PVC coated tarpaulin for truck and trailer cover, provide the exact trailer model dimensions including any protrusions or recessed areas, the operating climate range your fleet encounters, and whether flame retardant certification is required by your terminal or route regulations. Indicate if branded printing is needed on side curtains and the quantity per colour variant. Confirming whether you require finished covers with eyelets and hemming or roll stock for your own fabrication workshop determines both the lead time and the minimum order structure.
Frequently Asked Questions
Q: How do you verify GSM on arrival matches the quotation weight?
A: Every roll undergoes weight measurement during pre-shipment inspection, with results recorded against the quoted GSM. The material specification sheet accompanying each shipment states the verified weight, base fabric denier, and coating details. This eliminates the discrepancy between what was quoted and what arrives, a common issue when weight is only checked at the batch level rather than per roll.
Q: Can truck covers be cut to specific trailer model dimensions rather than generic sizes?
A: Yes. Covers are fabricated to the exact dimensions of your trailer model, including allowances for side curtain tracks, rear door clearance, and any body modifications. Providing the trailer manufacturer and model number allows precise patterning so the cover fits without excess fabric that would flap during transit and accelerate abrasion at contact points.
Q: What eyelet spacing and reinforcement options are available for tie-down points?
A: Standard configuration includes brass eyelets every 1 meter with 3cm enlarged aluminum alloy buttonholes at reinforced corners. Spacing can be adjusted for specific tie-down patterns, and additional reinforcement patches can be applied at high-load zones. The 5mm rope core inside the heat-sealed hem distributes strap tension across the full edge rather than concentrating it at individual eyelet points.
Q: How are welded seams tested to ensure they outlast the fabric at flex points?
A: Heat-sealed seams are produced using high temperature seamless edge wrapping with a 5mm rope core, avoiding adhesive bonds that crack under repeated flexing. In-process quality checks verify coating adhesion at seam zones during fabrication. This construction method addresses the common failure mode where welded joints separate before the main body of the PVC coated tarpaulin shows wear.